
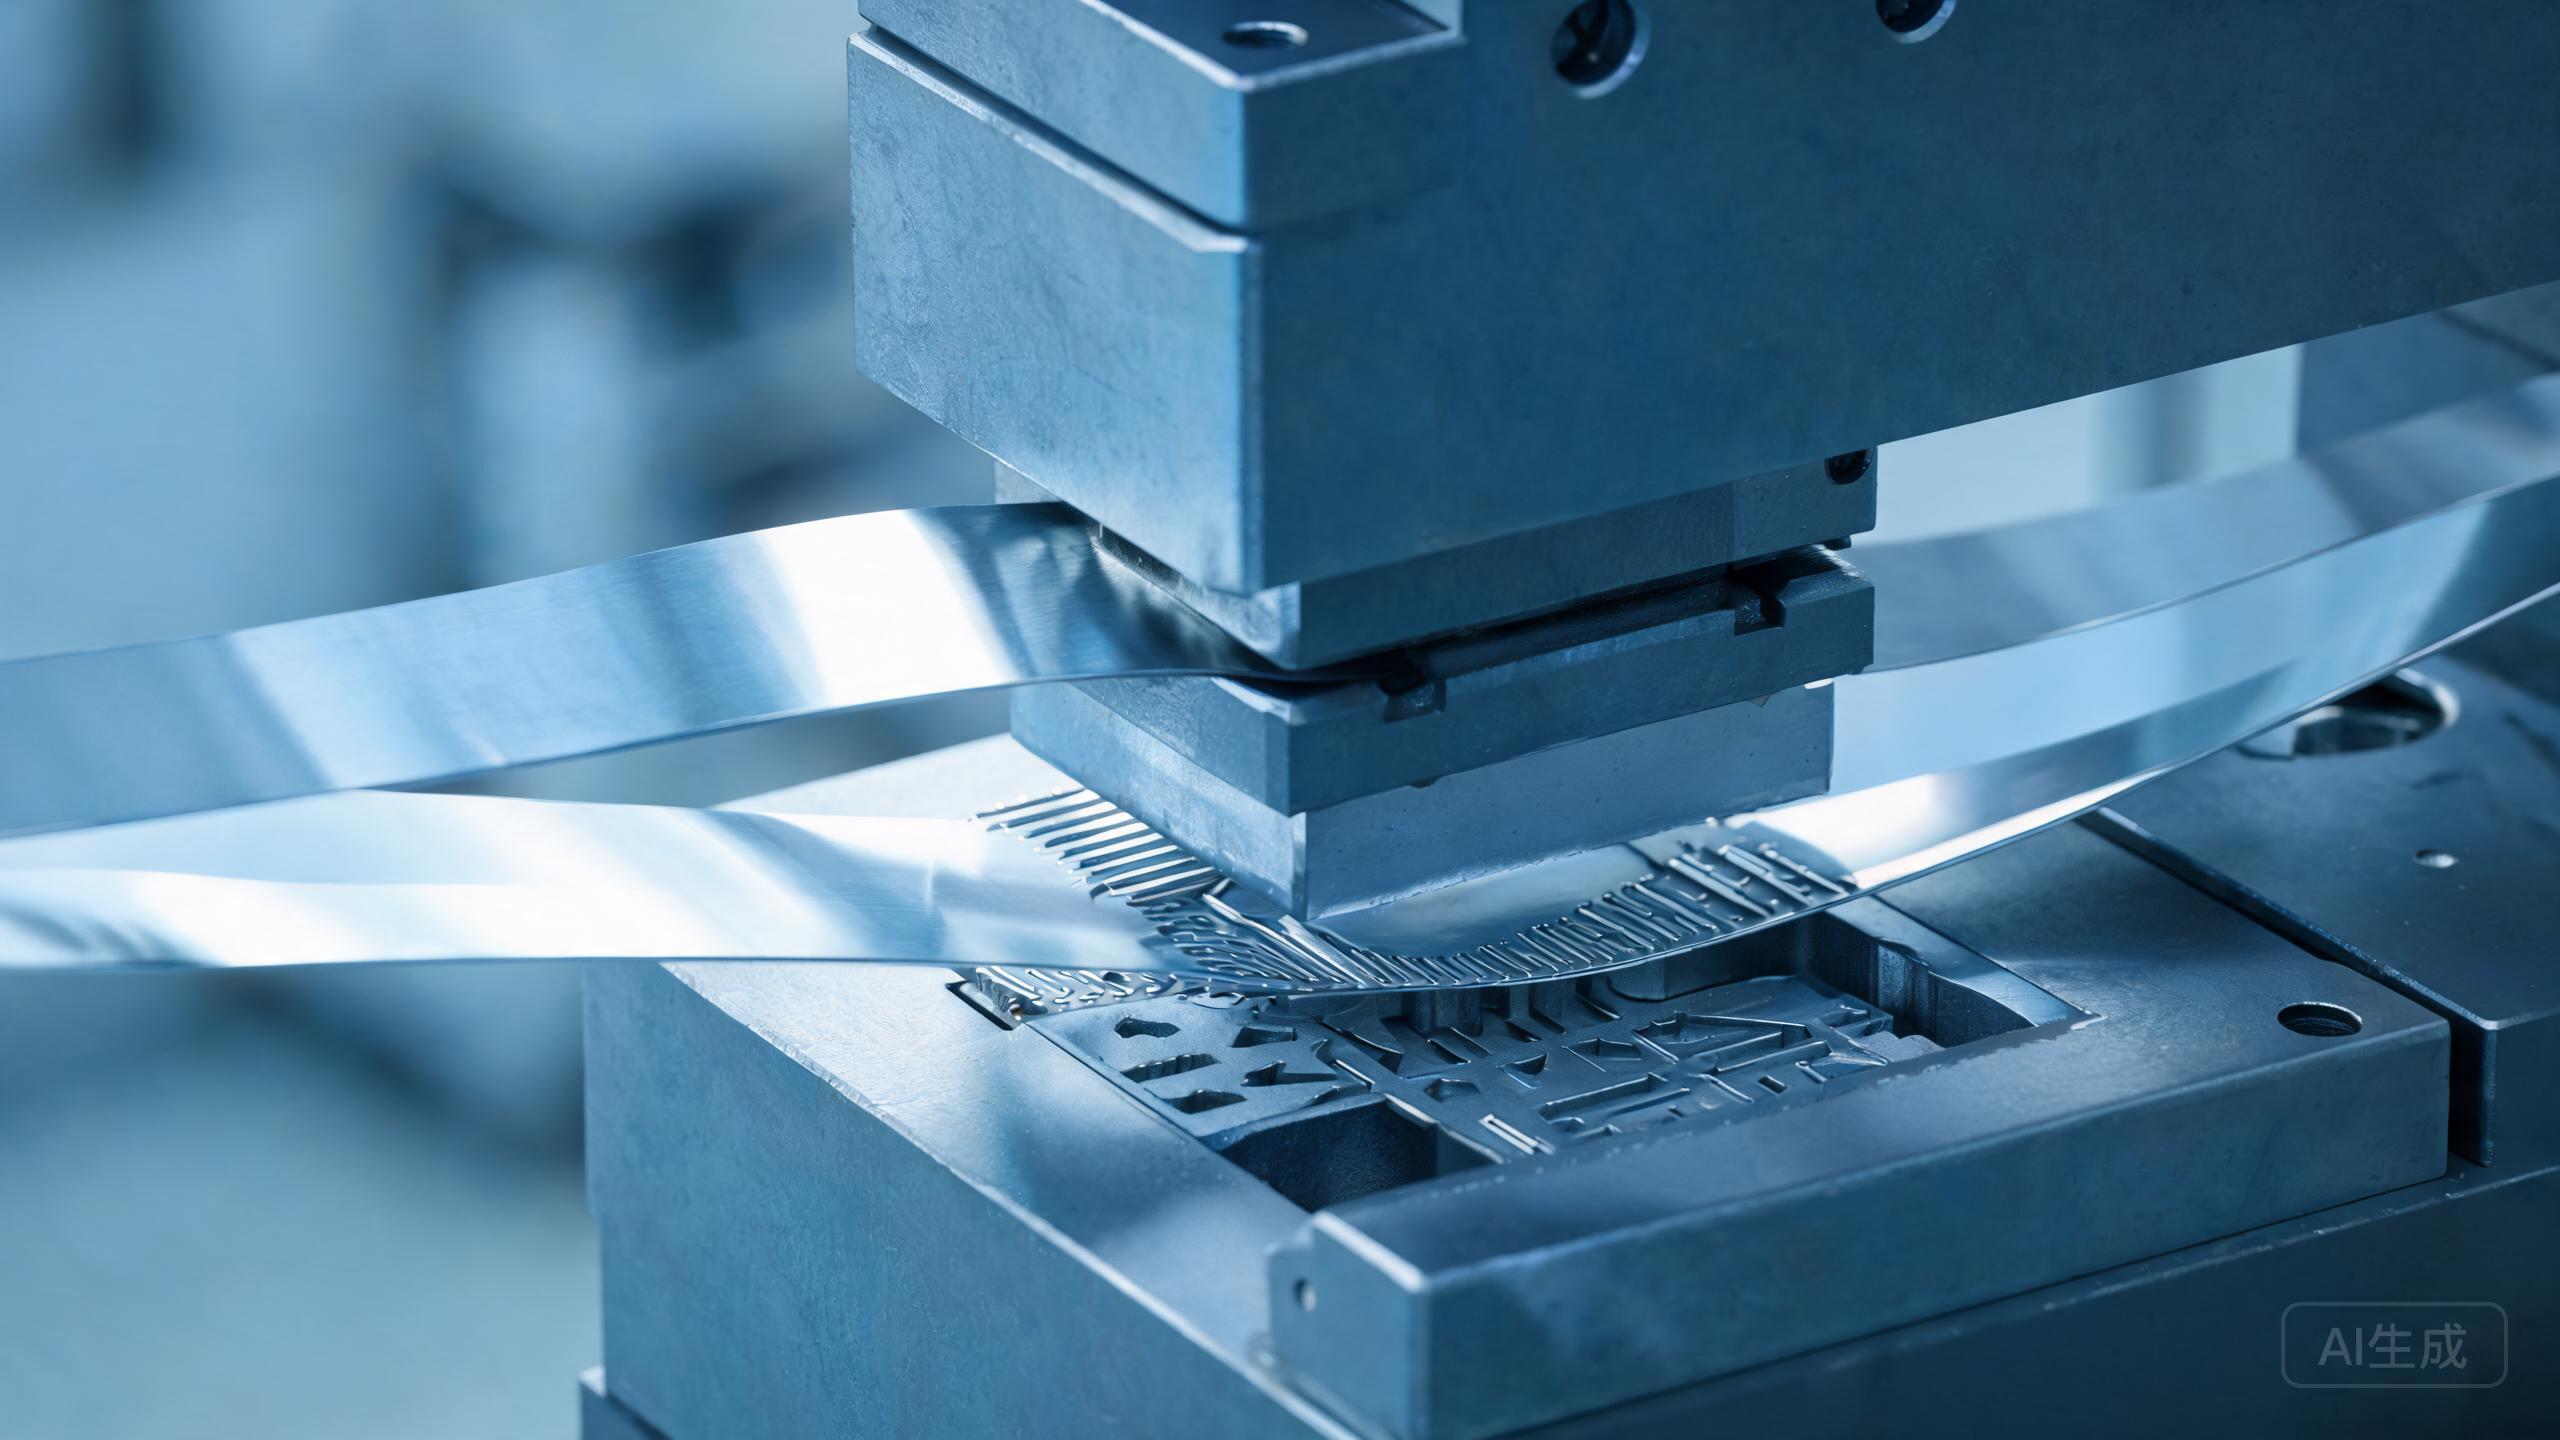
Short answer — Stamping ultra-thin stainless steel (below 0.2 mm) produces three dominant defects: wrinkling from insufficient blank-holder force, cracking from stress concentration at sharp radii or excessive thinning, and springback from the material’s high elastic recovery. Prevention requires matching temper to die design, using low punch speeds (200–500 mm/s), polished tooling, proper lubrication and over-bend compensation. Buyers must specify temper, thickness tolerance and grain direction before tooling is finalized.
This guide is written for stainless steel buyers, sourcing teams, engineers and product manufacturers. The purpose is not to declare one universal winner, but to turn a broad material question into a specification that a mill or service center can quote, process and inspect consistently.
Quick Comparison
| Defect | Root cause | Key countermeasure |
|---|---|---|
| Wrinkling | Blank-holder force too low; material rigidity insufficient | Increase BHF progressively; use vacuum or soft pad |
| Cracking | Sharp bend radius; local thinning >30%; wrong temper (hard) | Increase inner radius ≥2× thickness; switch to annealed or 1/4H |
| Springback | High elastic recovery of austenitic stainless | Over-bend 2–5°; use coining at bottom dead point; specify harder temper |
| Surface scratching | Die surface rough or contaminated; no protective film | Polish die to Ra ≤0.4 µm; apply PE film on strip |
| Dimensional drift | Residual stress from cold rolling; coil set | Stress-relieve or anneal before stamping; flatten strip |
The table is a starting point. Actual performance depends on the governing standard, delivered condition, dimensions, surface finish, fabrication route and service environment. Commercial names should never replace a complete purchase specification.
What Buyers Should Evaluate
- Temper selection: Annealed 304 (soft) has elongation ≥45% and is easiest to form without cracking, but shows maximum springback. 3/4 hard (HV ≥340) holds shape better but cracks at tight radii. Match temper to the part geometry: deep draws need annealed; flat springs need hard.
- Bend radius: For 0.1 mm strip, the minimum bend radius without cracking is approximately 1.0 mm for annealed 304 and 2.0 mm for half-hard. Never design a sharp internal corner on ultra-thin stainless — it will crack.
- Grain direction: Bending across the rolling direction (cross-grain) allows tighter radii than bending along the rolling direction (parallel-grain). Specify grain direction on the drawing for critical bend parts.
- Punch speed: Research on 0.1 mm SS304 bipolar plates shows that punch speeds of 200–500 mm/s produce comparable thinning (23–25%), but speeds above 800 mm/s increase maximum thinning to 26%+ and raise fracture risk at channel corners.
- Lubrication: Use a low-friction stamping lubricant rated for stainless steel. Dry stamping of ultra-thin 304 causes galling, tool buildup and surface scratches that cannot be repaired.
For production orders, share the end use rather than requesting a grade or finish in isolation. A supplier can then review corrosion exposure, forming severity, welding, visual requirements and packing before material is cut. This early review is usually less expensive than correcting a rejected shipment or unstable production trial.
Common Purchasing Mistakes
- Ordering full-hard temper for a part with a 0.5 mm bend radius — the strip cracks at every bend and the entire stamping run is scrapped
- Not specifying grain direction — the supplier ships random grain orientation, and bend parts crack inconsistently across batches
- Accepting strip without protective film — handling and die contact scratch the surface, and these scratches cannot be polished out on 0.05 mm material
- Using a die designed for 0.3 mm material on 0.1 mm strip — the clearance is too large, causing wrinkling, edge curling and dimensional instability
Verification: Before bulk production, run a 50-piece trial stamping with the actual coil. Measure springback angle, check for micro-cracks at bend radii under 10× magnification, and verify thickness at the thinnest point does not exceed 25% reduction from nominal. Require EN 10204 3.1 MTC confirming the temper and mechanical properties match the purchase specification.
Recommended RFQ Wording
Specify: grade (304 / UNS S30400), nominal thickness and minimum acceptable thickness, tolerance band per ASTM A240, temper (annealed / 1/4H / 1/2H / 3/4H with HV range), surface finish (2B / BA), edge condition (slit / round-trimmed), grain direction (parallel / cross to bending axis), protective film (double-sided PE anti-static), coil ID and weight, and stamping application description (bend radius, draw depth, part geometry).
Also include order quantity, acceptable quantity variation, destination, required delivery date and whether partial shipments are allowed. If a requirement is critical, make it measurable and place it on the purchase order rather than only in an email conversation.
How Still Steel Supports the Project
Still Steel supplies stainless steel coil, strip and sheet and provides slitting, cut-to-length, brushing, polishing and protective-film services. We can compare available mill material with your drawing, prepare trial quantities and preserve heat-number traceability through service-center processing.
Send the grade, dimensions, annual volume and application to vip@still-steel.com, or discuss the requirement on WhatsApp, or request a quote online.
Frequently Asked Questions
Why does ultra-thin stainless steel wrinkle during stamping?
Wrinkling occurs when blank-holder force is too low for the material’s minimal rigidity. At 0.1 mm thickness, even slight uneven compression causes the sheet to fold. Increase blank-holder pressure progressively and use a polished die surface with proper lubrication.
How do I reduce springback in ultra-thin 304 stamping?
Over-bend by 2–5° to compensate for elastic recovery, use bottom-dead-point coining in the die, and specify 3/4 hard or full-hard temper instead of annealed. Lower punch speed also reduces springback variation.
What punch speed is safe for stamping 0.1 mm stainless strip?
For 0.05–0.15 mm 304 strip, keep punch speed at 200–500 mm/s. Speeds above 800 mm/s increase strain-rate effects and the risk of cracking at channel corners and side-boss roots.
Technical References
- ASTM A240/A240M stainless steel sheet and strip
- ASTM A666 work-hardened stainless strip temper conditions
- EN 10088-2 stainless steel strip technical conditions
Reference documents support general selection and fabrication principles. The final material decision must follow the applicable contract, standard, regulation and engineering review for the specific product.