
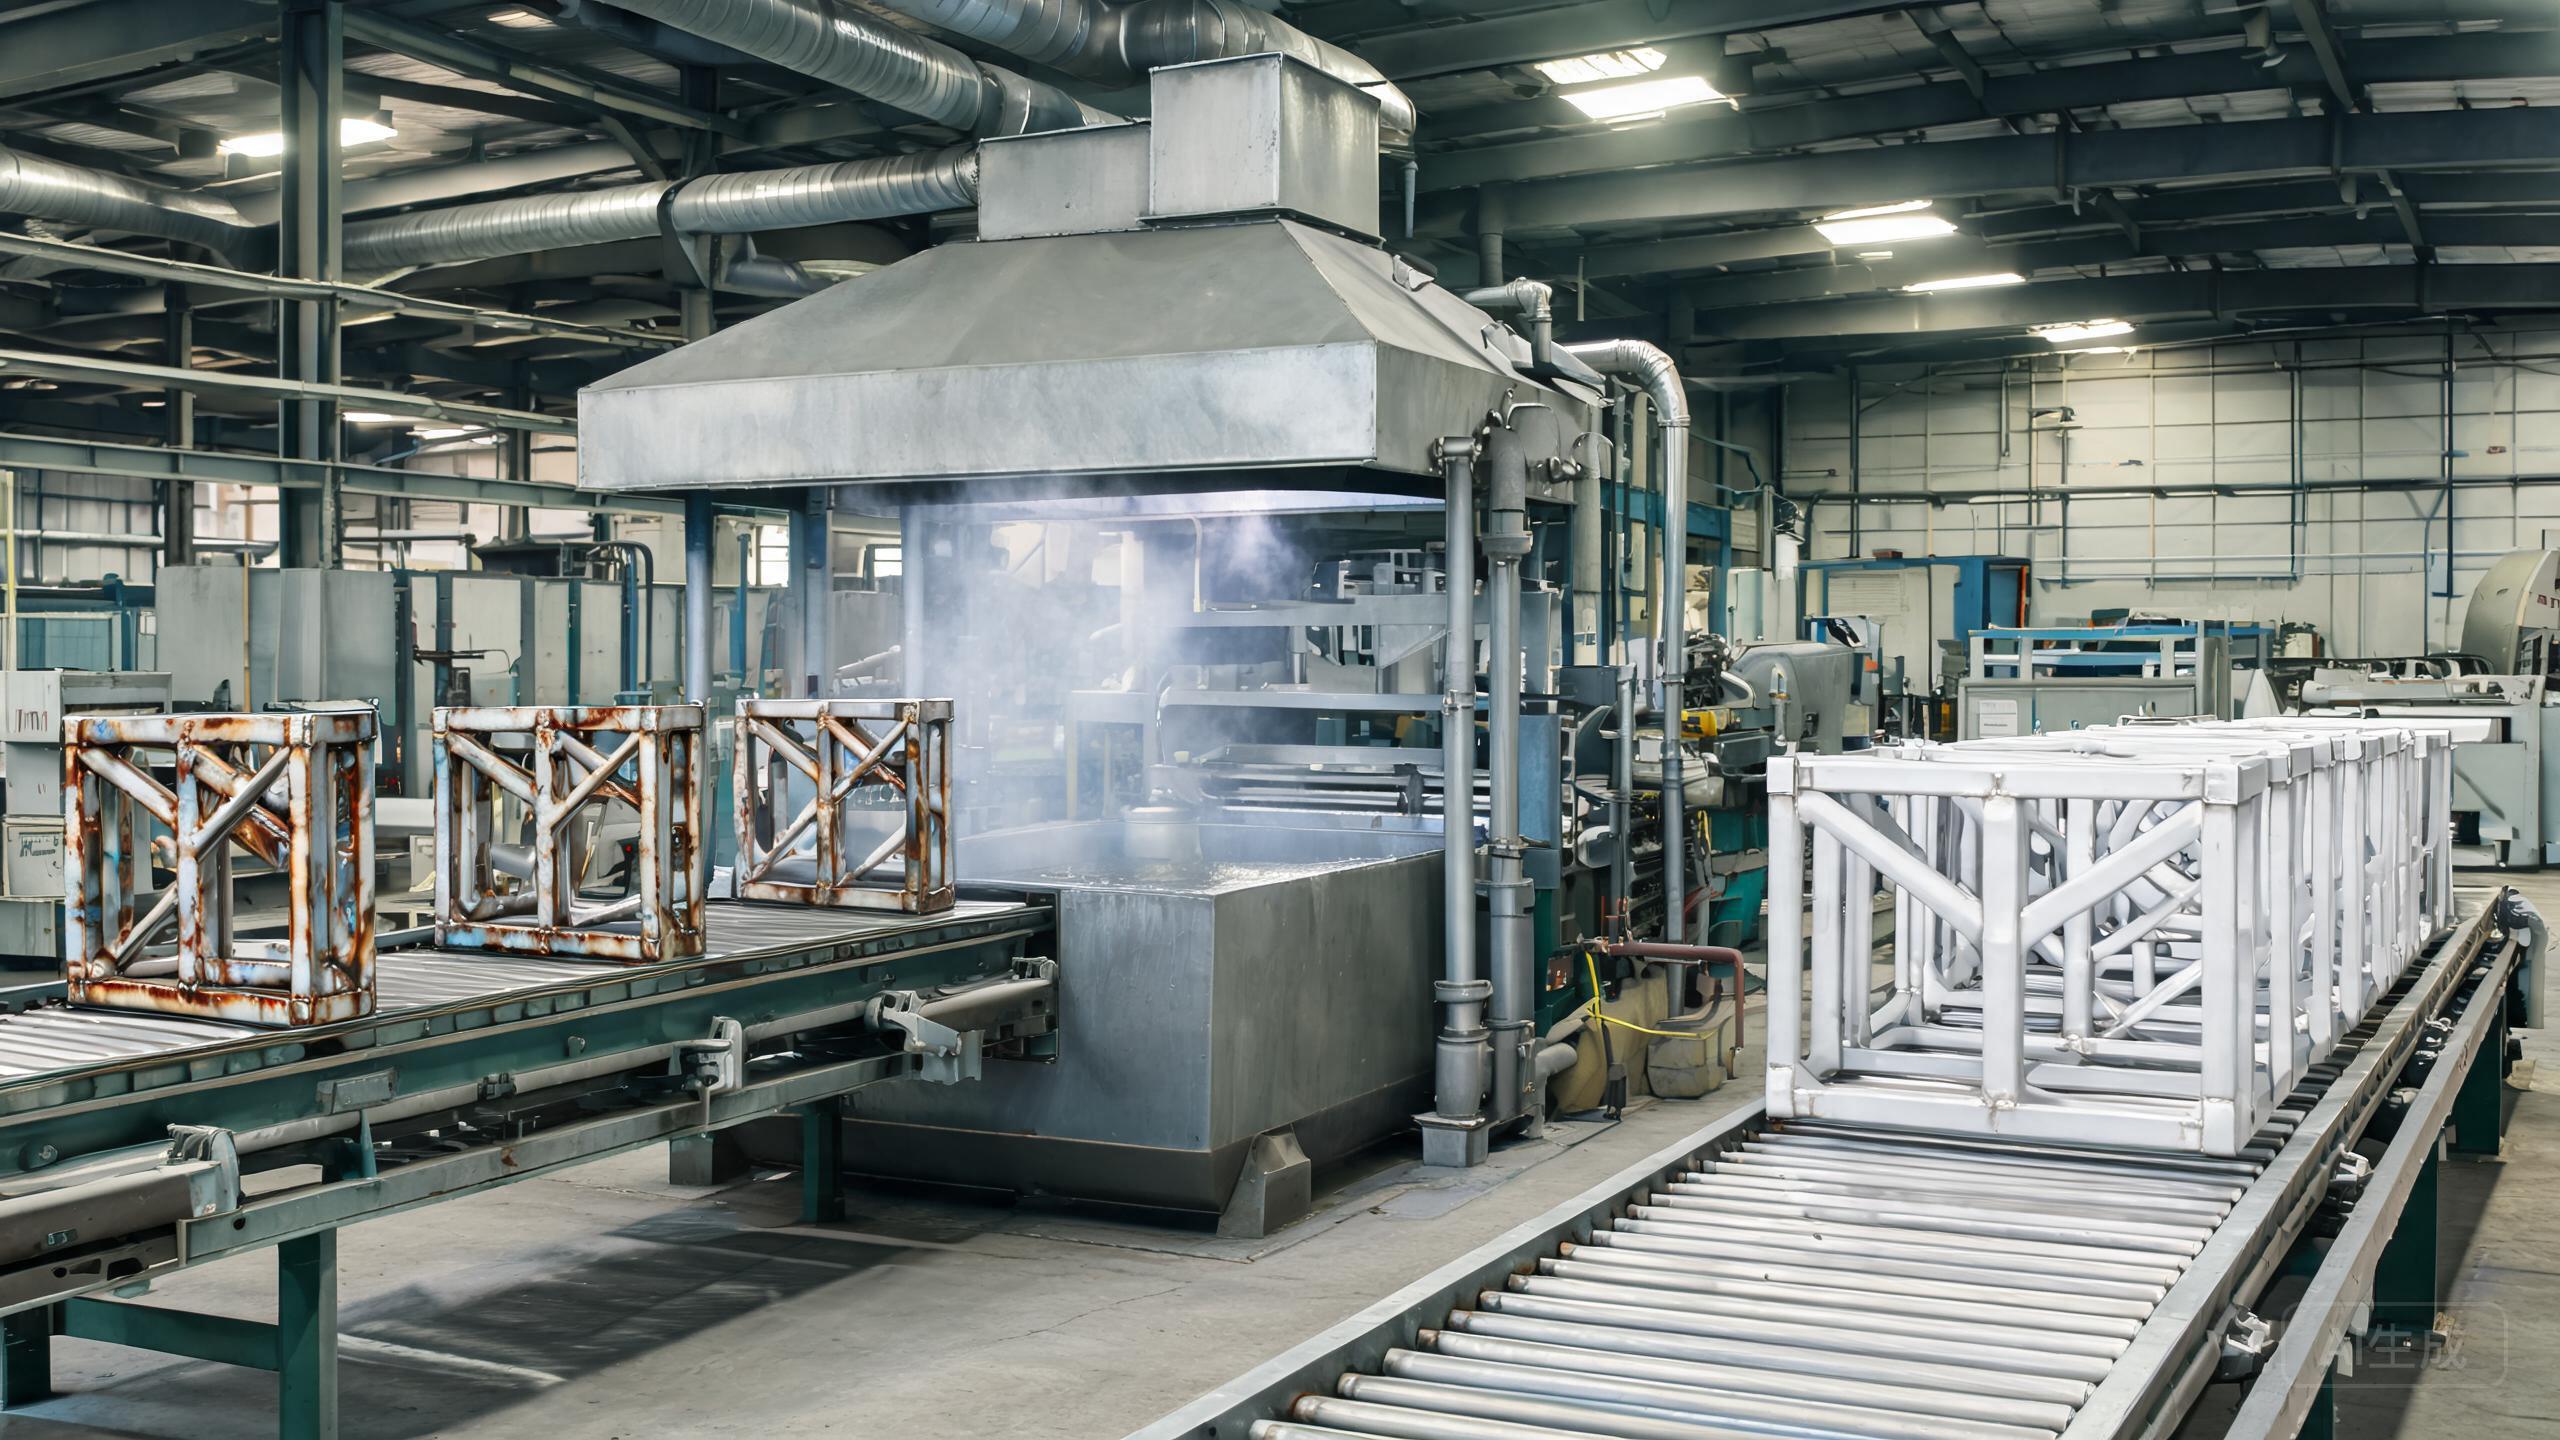
Short answer: Pickling removes scale, weld heat tint and embedded iron from stainless steel surfaces using strong acids (typically nitric + HF mixtures), while passivation dissolves free iron and promotes the chromium-rich passive layer without visibly changing the surface. Pickling is required after hot operations; passivation is specified after fabrication, machining or handling contamination.
This guide is written for stainless steel buyers, sourcing teams, engineers and product manufacturers. The purpose is not to declare one universal winner, but to turn a broad material question into a specification that a mill or service center can quote, process and inspect consistently.
Quick Comparison
| Option | Key point | Typical use or decision |
|---|---|---|
| Pickling (Nitric + HF or equivalent) | Aggressive descaling, removes heat tint | After welding, hot forming or heavy scale |
| Nitric acid passivation | Free-iron removal, ASTM A967 options | Valves, pumps, food and pharma equipment |
| Citric acid passivation | Safer chemistry, avoids nitric disposal | Medical devices, aerospace components, cleaner production |
The table is a starting point. Actual performance depends on the governing standard, delivered condition, dimensions, surface finish, fabrication route and service environment. Commercial names should never replace a complete purchase specification.
What Buyers Should Evaluate
- Specify the governing passivation standard (ASTM A967, ASTM A380 or ISO 15730), not just “passivate”.
- Agree acceptance criteria: visual, copper sulfate test, salt spray, humidity or ferricyanide spot test.
- Require a certificate of compliance with the cleaning, passivation and rinse steps for regulated industries.
To avoid specifying a surface treatment that masks an underlying problem, first check why stainless typically loses its passive layer by reading why stainless steel rusts and the discoloration profile left after welding — both situations decide whether pickling or passivation is the right remedy.
For production orders, share the end use rather than requesting a grade or finish in isolation. A supplier can then review corrosion exposure, forming severity, welding, visual requirements and packing before material is cut. This early review is usually less expensive than correcting a rejected shipment or unstable production trial.
Common Purchasing Mistakes
- Passivating without first removing heat tint, oil, grease or masking tape residue
- Using carbon-steel tools or handling equipment after passivation and re-contaminating the surface
- Trusting “we usually passivate” without a standard, a written procedure or a test
These mistakes are avoidable when drawings, approved samples, inspection methods and certificate requirements are agreed before production. For visual products, retain a signed master sample. For functional dimensions, define where and how measurements will be taken.
Recommended RFQ Wording
Reference the passivation or pickling standard by number, list required post-treatment tests, declare whether the treatment must be done before or after final assembly, and name the certificate (mill certificate or independent) to be issued.
Also include order quantity, acceptable quantity variation, destination, required delivery date and whether partial shipments are allowed. If a requirement is critical, make it measurable and place it on the purchase order rather than only in an email conversation.
How Still Steel Supports the Project
Still Steel supplies stainless steel coil, strip and sheet and provides slitting, cut-to-length, brushing, polishing and protective-film services. We can compare available mill material with your drawing, prepare trial quantities and preserve heat-number traceability through service-center processing.
Send the grade, dimensions, annual volume and application to vip@still-steel.com, or discuss the requirement on WhatsApp.
Frequently Asked Questions
Do all stainless parts need pickling?
No. Mill-finished material from a reputable mill usually arrives with a passive surface. Pickling is specified after welding, hot forming, heat tint or heavy handling contamination.
Is citric passivation as effective as nitric?
For many austenitic and duplex grades, citric acid passivation is a recognized route per ASTM A967. Validation testing should follow the project standard.
Can a brushed finish be passivated?
Yes, but passivation after brushing may alter appearance slightly. Agree a master sample or pre-production approval before full batches.
Technical References
Reference documents support general selection and fabrication principles. The final material decision must follow the applicable contract, standard, regulation and engineering review for the specific product.